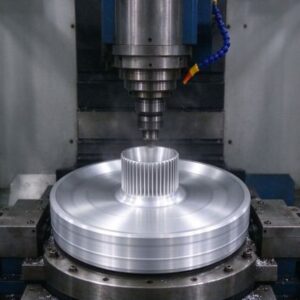
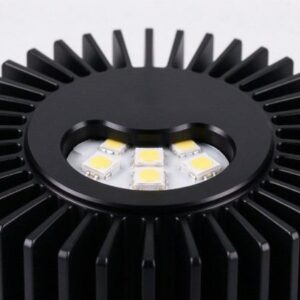
এলইডি হিটসিঙ্কের জন্য অ্যালুমিনিয়াম ডিস্ক
| স্পেসিফিকেশন | মান |
| মেজাজ | ও (নরম, স্পিনিং) / H14-H24 (মুদ্রাঙ্কন, অনমনীয় প্লেট) |
| পুরুত্ব | 0.5-6 মিমি |
| ব্যাস | 50-500 মিমি (ফাঁকা আকারে কাটা) |
| তাপ পরিবাহিতা | ~220–230 W/mK (1xxx) |
| সহনশীলতা | ব্যাস ±0.2–0.5 মিমি, প্রতি বিশেষ বেধ |
| অ্যাপ্লিকেশন | LED কাপ কাটা, বেস প্লেট, বাল্ব/রাস্তা/হাই-বে হিট সিঙ্ক |
এলইডি হিটসিঙ্কের জন্য অ্যালুমিনিয়াম ডিস্ক
ভূমিকা
এলইডি হিটসিঙ্কের জন্য একটি অ্যালুমিনিয়াম ডিস্ক উচ্চ-বিশুদ্ধ অ্যালুমিনিয়ামের একটি বৃত্তাকার ফাঁকা। (প্রায়ই 1050, 1060 বা 1100) যে আলো নির্মাতারা স্পিন, ছাপ, একটি LED luminaire তাপ-প্রসারণ শরীরের মধ্যে গভীর আঁকা বা মেশিন.
LEDs হল সংবেদনশীল ডিভাইস: যদি তারা তাপ কমাতে না পারে, তাদের সংযোগস্থলের তাপমাত্রা বৃদ্ধি পায়, হালকা আউটপুট ড্রপ, রঙ পরিবর্তন এবং জীবন সংক্ষিপ্ত.
অ্যালুমিনিয়াম ডিস্ক হল কাঁচামাল যা তাপ সিঙ্কে পরিণত হয়, লাইট-কাপ শেল এবং বেস প্লেট যা LED বোর্ড থেকে আশেপাশের বাতাসে তাপ সঞ্চালন করে.
LED তাপ ব্যবস্থাপনার জন্য, অ্যালুমিনিয়াম সবচেয়ে বিকল্প বীট.
এটা হালকা, কম খরচে, স্পিন এবং স্ট্যাম্প করা সহজ, জারা প্রতিরোধী, এবং - এর বিশুদ্ধ 1xxx আকারে - একটি ভাল তাপ পরিবাহী.
এই নির্দেশিকা ব্যাখ্যা করে যে এলইডি হিটসিঙ্কের জন্য কোন অ্যালুমিনিয়াম ডিস্ক ব্যবহার করা হয়, কেন খাঁটি মিশ্র ধাতুগুলি তাপের জন্য শক্তিশালীগুলিকে ছাড়িয়ে যায়, tempers এবং মাপ উপলব্ধ, কিভাবে ফাঁকা তৈরি এবং গঠিত হয়, প্রধান luminaire অ্যাপ্লিকেশন, anodizing এবং পৃষ্ঠ সমাপ্তি, তাপ নকশা, মান নিয়ন্ত্রণ, মূল্য এবং অর্ডার, এবং একটি মূল স্পেসিফিকেশন টেবিল.

LED Heatsinks জন্য একটি অ্যালুমিনিয়াম ডিস্ক কি??
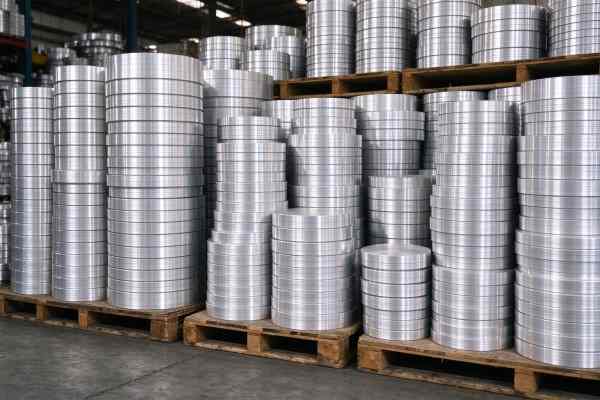
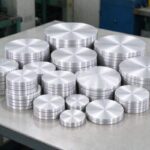
একটি অ্যালুমিনিয়াম ডিস্ক (একটি অ্যালুমিনিয়াম বৃত্ত বা ফাঁকা বলা হয়) অ্যালুমিনিয়াম কয়েল থেকে কাটা একটি গোলাকার শীট. LED হিটসিঙ্কের জন্য এটি সাধারণত 0.5-6 মিমি পুরু এবং মোটামুটি থেকে 50 মিমি থেকে কয়েকশ মিলিমিটার ব্যাস, আলোর উপর নির্ভর করে.
তারপর ডিস্কটি নিচের দিকে রূপান্তরিত হয় - একটি কাপে কাটা হয়, একটি অগভীর প্যান মধ্যে স্ট্যাম্পড, অথবা মেশিনযুক্ত—একটি স্পটলাইটের তাপ-প্রসারণকারী শেল হয়ে উঠতে, ডাউনলাইট, বাল্ব বা রাস্তার ফিক্সচার.
একবারে দুটি বৈশিষ্ট্যের জন্য ডিস্কটি বেছে নেওয়া হয়: তাপ পরিবাহিতা এবং গঠনযোগ্যতা.
ক 1050/1060/1100 ডিস্ক ভাল তাপ সঞ্চালন করে (বিশুদ্ধ অ্যালুমিনিয়াম প্রায় 220-230 W/mK) এবং ক্র্যাকিং ছাড়াই স্পিন বা ডিপ-ড্র করতে ও মেজাজে যথেষ্ট নরম.
শক্তিশালী খাদ যেমন 3003 বা 5052 কঠোর এবং আরো জারা-প্রতিরোধী কিন্তু কম ভাল তাপ সঞ্চালন; এগুলি বিশুদ্ধ তাপ ছড়ানোর পরিবর্তে যান্ত্রিকভাবে চাহিদাপূর্ণ অংশগুলির জন্য সংরক্ষিত.
সবচেয়ে সাধারণ ফাঁকা হল 1050 অ্যালুমিনিয়াম বৃত্ত; শক্ত গঠিত অংশ কখনও কখনও ব্যবহার 3003 অ্যালুমিনিয়াম বৃত্ত.
এই শব্দটি হালকা কাপে কাটা ছোট পাতলা ডিস্ক এবং বেস প্লেটে তৈরি করা বড় পুরু চাকতি উভয়কেই কভার করে।.
যা তাদের একত্রিত করে তা হল ডিস্কটি হল প্রারম্ভিক ফাঁকা, সমাপ্ত অংশ না: আলো প্রস্তুতকারক এটি গঠন করে, এটা anodizes, LED বোর্ড এবং ড্রাইভার মাউন্ট করে, এবং ল্যুমিনায়ার পাঠায়.
এই কারণেই বিশেষ নির্ভুলতা গুরুত্বপূর্ণ - একটি ডিস্ক যা স্পিনিং লাইনে খুব পাতলা ফাটল।, একটি যে সমতল নয় eccentrically রান, এবং একটি ভুল সংকর ধাতু উচ্চ ক্ষমতার LED উৎপন্ন করে তাপ ছাড়তে পারে না.
কেন এলইডি তাপ ব্যবস্থাপনার জন্য অ্যালুমিনিয়াম?
ভাল তাপ পরিবাহিতা: বিশুদ্ধ 1xxx অ্যালুমিনিয়াম প্লাস্টিক বা ডাই-কাস্ট জিঙ্কের চেয়ে অনেক ভালো তাপ সঞ্চালন করে.
হালকা ওজন: তামার ঘনত্বের প্রায় এক তৃতীয়াংশ, recessed এবং retrofit ফিক্সচার জন্য গুরুত্বপূর্ণ.
স্পিন এবং পাতলা মধ্যে স্ট্যাম্প সহজ, পাতলা দেয়ালের হালকা কাপ এবং প্যান.
তামার তাপ সিঙ্কের তুলনায় কম খরচে এবং ব্যাপকভাবে উপলব্ধ.
প্রাকৃতিকভাবে জারা-প্রতিরোধী এবং তাপ অপচয় এবং নিরোধকের জন্য অ্যানোডাইজিং গ্রহণ করে.
পুনর্ব্যবহারযোগ্য এবং আলো শিল্পের খরচ এবং ভলিউম লক্ষ্যগুলির সাথে সামঞ্জস্যপূর্ণ.
তামা অ্যালুমিনিয়ামের চেয়ে ভাল সঞ্চালন করে তবে ভারী এবং আরও ব্যয়বহুল; প্লাস্টিক সস্তা কিন্তু একটি অন্তরক. অ্যালুমিনিয়াম মিষ্টি জায়গায় বসে: একটি উচ্চ শক্তি LED ঠান্ডা করার জন্য যথেষ্ট পরিবাহী, সিলিং ফিক্সচারের জন্য যথেষ্ট আলো, এবং একটি ভোক্তা বাল্বের জন্য যথেষ্ট সস্তা. এই কারণেই বাজারে প্রায় প্রতিটি LED হিট সিঙ্ক শেল-বিশেষ করে কাটা বা স্ট্যাম্পযুক্ত গোলাকারগুলি-একটি অ্যালুমিনিয়াম ডিস্ক হিসাবে শুরু হয়.
প্লাস্টিকের সাথে তুলনা, অ্যালুমিনিয়াম ভাল মাত্রার তাপ আদেশ সঞ্চালিত, তাই একটি প্লাস্টিকের বাল্বের শরীর তাপকে আটকে রাখে এবং LED লাইফকে ছোট করে.
ডাই-কাস্ট অ্যালুমিনিয়ামের সাথে তুলনা করা হয়, একটি কাটা 1050 কাপ পাতলা, মসৃণ এবং সরঞ্জাম সস্তা, এবং ছিদ্রযুক্ত ডাই-কাস্টের চেয়ে ভাল পরিচালনা করে.
তামার সঙ্গে তুলনা, অ্যালুমিনিয়াম ওজনের প্রায় এক তৃতীয়াংশ এবং অনেক সস্তা, এবং তাপমাত্রায় একটি ছোট LED সিঙ্ক দেখতে পায়, পরিবাহিতা ব্যবধান একটি হালকা অ্যালুমিনিয়াম শেল অনুমতি দেয় বৃহত্তর পৃষ্ঠ এলাকা দ্বারা গঠিত হয়.
যা খাদ? তাপ পরিবাহিতা বনাম শক্তি
| খাদ | প্রায়. তাপ পরিবাহিতা (W/mK) | চরিত্র | LED heatsinks জন্য ব্যবহার করুন |
| 1050 / 1060 | ~225-230 | বিশুদ্ধ, খুব নরম, সর্বোচ্চ পরিবাহিতা | কাটা কাপ, বেস প্লেট, তাপ স্প্রেডার্স |
| 1100 | ~218 | সামান্য Cu সঙ্গে বিশুদ্ধ, নরম, ভাল গঠনযোগ্যতা | স্ট্যাম্পড প্যান, হালকা কাপ |
| 3003 | ~160–190 | Mn খাদ, শক্তিশালী, কড়া | mechanically demanding formed parts |
| 5052 | ~130 | এমজি খাদ, শক্তিশালী, জারা প্রতিরোধী | structural housings, not primary heat sink |
নিয়মটা সহজ: for the part that spreads LED heat, choose the purest soft alloy that still forms.
As alloying elements are added (Mn in 3003, Mg in 5052), strength and corrosion resistance rise but thermal conductivity falls.
ক 5052 heat sink looks strong but moves heat poorly; ক 1050 disc conducts well but may be too soft for a structural wall. Most spun LED cups are 1050/1060 ও, which balances both.
Reflective inner surfaces for some luminaires use a 5052 উচ্চ-প্রতিফলিত মিরর শীট; general structural sheet can come from the 5000 সিরিজ অ্যালুমিনিয়াম শীট পরিসীমা.
ব্যবহারিক পরামর্শ: do not over-specify. A lighting buyer asked for “strongest aluminum” may end up with 5052, which feels premium but moves heat about 40% less well than 1050 and runs the LED hotter.
Reserve 3003/5052 for the few parts that really need mechanical stiffness or outdoor corrosion, এবং ব্যবহার করুন 1050/1060 for the heat-spreading cup and base.
If in doubt, a sample in each alloy with a simple temperature test under the same LED and current settles the question faster than datasheets.
মেজাজ: O for Spinning, H for Stiffness
হে মেজাজ (annealed, নরম) is the standard for LED discs that will be spun or deep-drawn.
A soft disc flows under the spinning roller without cracking, which is essential for thin light cups and tapered shells.
H14/H24 or half-hard tempers are used when the disc is stamped into a shallow pan that must keep its shape, or when the finished part needs stiffness rather than deep forming.
Getting the temper wrong is a classic defect: a half-hard disc spun into a deep cup cracks at the base, while an O disc used as a rigid base plate is too soft and dents.
The blank supplier therefore matches the temper to the forming process—O for spinning and deep drawing, H for shallow stamping and rigid plates—and the converter trials a sample before volume.
Spinning in particular is temper-sensitive. An O disc needs enough annealed softness to flow under the roller without springback, but fully annealed stock that is too soft can wrinkle or tear on a deep draw.
The mill controls the anneal to a consistent temper, and the spinning line sets roller pressure and feed speed to match.
Variation in temper between batches is a common cause of cracked cups, which is why a mill certificate on temper—not just alloy—is part of the spec.
সাধারণ বিশেষ উল্লেখ
| প্যারামিটার | সাধারণ পরিসীমা |
| খাদ / মেজাজ | 1050 / 1060 / 1100, ও (নরম) or H14/H24 |
| পুরুত্ব | 0.5-6 মিমি; spun cups ~0.6–2 mm, base plates 2–6 mm |
| ব্যাস | 50-500 মিমি, cut to the cup/base blank size |
| সমতলতা | সমতল, burr-মুক্ত প্রান্ত, সামঞ্জস্যপূর্ণ ব্যাস |
| পৃষ্ঠতল | মিল ফিনিস; anodized করা যেতে পারে, blasted or brushed downstream |
| কাটিং | sheared or blanked circle, controlled burr and edge |
| সহনশীলতা | ব্যাস ±0.2–0.5 মিমি, প্রতি বিশেষ বেধ |
Blank diameter is calculated from the finished cup dimensions using the surface area of the drawn part—a deep, thin cup needs a larger blank than a shallow pan.
Thickness depends on thermal mass and wall thinning during spinning: a thin cup uses 0.6–1.5 mm, while a solid base plate under a high-power COB LED uses 3–6 mm to spread heat.
Blank sizing is the first engineering step. The spun cup thins as it forms, so the disc must be thick enough to leave a minimum wall after drawing.
Buyers often work backwards from the cup drawing: required wall thickness, cup diameter and depth set the blank diameter and starting gauge.
Leaving too large a blank creates trim waste; too small a blank splits at the rim. Because circle cutting is cheap, it is normal to cut a few blank sizes, spin samples, and lock the diameter that gives a clean cup with the least scrap.
কয়েল থেকে ডিস্ক পর্যন্ত: How Blanks Are Made
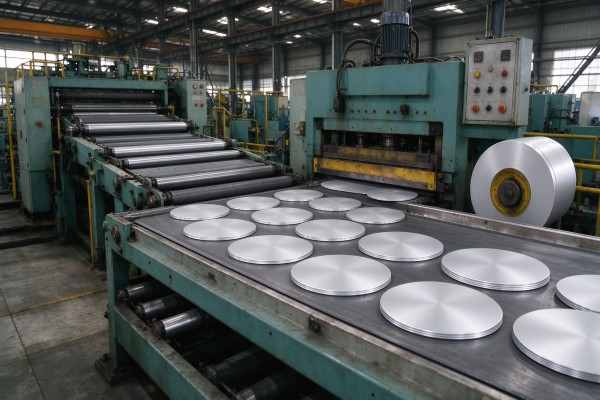
LED heat-sink discs start from cold-rolled aluminum coil in the chosen alloy and temper.
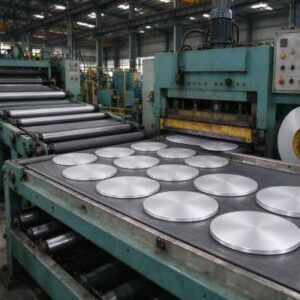
কুণ্ডলী uncoiled হয়, সমতল, and blanked on a circle-cutting line—either sheared with round dies or punched in a blanking press—into round discs of the target diameter.
The edge is controlled for burr and the disc is stacked, interleaved if needed, and inspected for flatness and gauge.
The key quality points are flatness (a warped disc spins eccentrically), প্রান্ত burr (which causes cracking in forming), গেজ ধারাবাহিকতা, এবং পৃষ্ঠের পরিচ্ছন্নতা.
Because the blank is spun into a thin shell, even small gauge variation shows up as uneven wall thickness or splitting.
A good circle line cuts clean, সমতল, burr-free discs that the converter can run directly on the spinning or stamping machine.
Yield on a circle line depends on nesting: cutting the maximum number of discs from a coil width to minimize scrap.
For large diameters the trim between circles is the main cost, so specifying a diameter that nests well on a standard coil width reduces price.
Tolerance and edge condition are specified per application—anodizing-grade discs need a clean, scratch-free surface because anodizing reveals every rolling mark, while spun cups mainly need flatness and burr control.

গঠন: Spinning vs Stamping vs CNC
Three processes turn a disc into a heat sink. Spinning clamps the disc over a mandrel on a lathe and rollers press it into a tapered cup—ideal for thin, round LED light cups and spotlights, and cheap for medium and large runs.
Stamping and deep drawing press the disc in a die into shallow pans and flatter base plates.
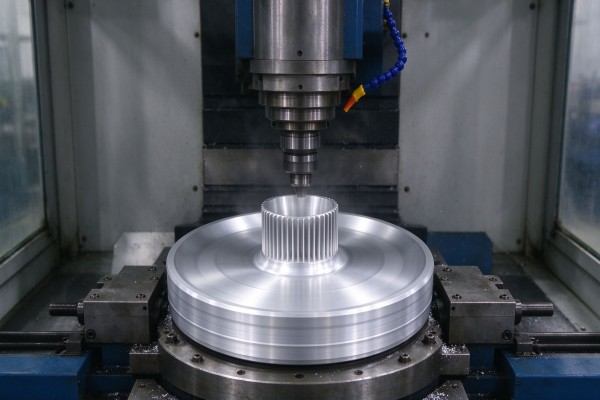
CNC machining is used for high-power finned heat sinks cut from solid disc or plate, where precise fin geometry matters.
Spinning is the dominant process for round LED heat cups because it is fast, tooling is cheap, and it produces the tapered, thin-wall shell that lights need.
ও-মেজাজ 1050/1060 disc flows smoothly under the roller. Stamping suits flat plates and shallower parts; CNC suits high-power, finned industrial and street heat sinks where thermal performance is engineered rather than shaped.
The choice of process drives the disc spec. Spinning wants a soft O disc with a clean, burr-free edge and good flatness; stamping wants consistent gauge so the die does not overload;
CNC wants a thicker plate or disc with stable thickness and a clean, machinable surface.
Telling the blank supplier which process the disc will go into prevents the most common mismatch—a stamping-grade disc that is too soft, or a spinning disc with an edge burr that cracks under the roller.

আবেদন: LED Spotlights and Downlights
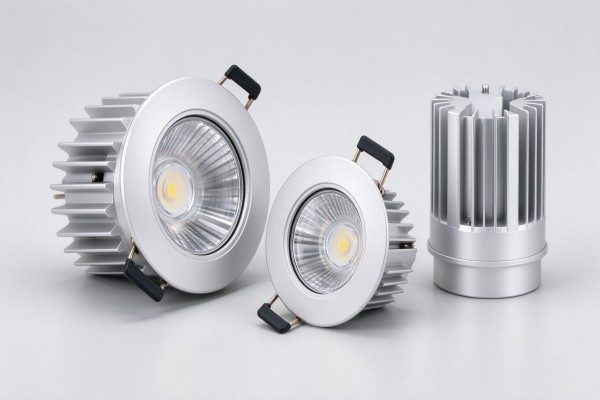
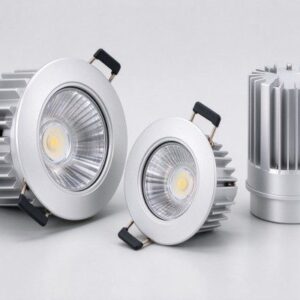
The classic spun aluminum heat cup is the body of an LED spotlight, PAR lamp or downlight.
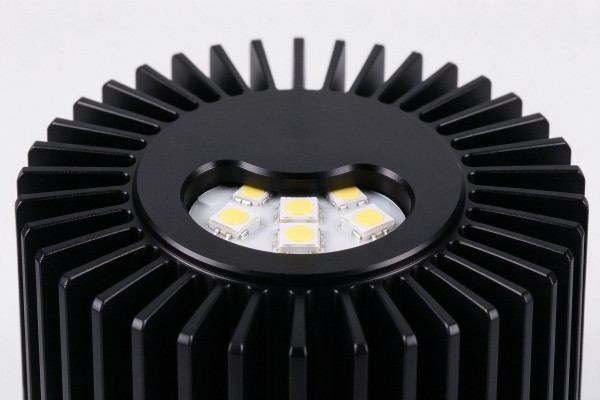
The disc is spun into a tapered shell that doubles as the heat sink and the lamp body: the LED board mounts on the flat back or base, heat conducts through the aluminum wall, and the outer surface (often finned or fluted) radiates to the air.
This is why the cup must be thermally conductive and dimensionally round.
For recessed downlights and spotlights, weight and thermal performance both matter—the fixture hangs in a ceiling and must cool the LED without a fan.
ক 1050/1060 O disc spun thin gives low mass and good conduction; the outside is often anodized black or white to match the interior.
Consistent blank diameter and flatness keep the spun cups concentric and the fixture cosmetic.
Recessed downlights are a thermal tight spot: the fixture sits inside a ceiling void with little air flow, so the spun cup must shed heat conductively to its outer surface and through the trim.
A thin, low-mass cup looks elegant but can run hot; makers balance wall thickness, fluting and anodizing to keep junction temperature within the LED’s rating.
Because these cups are visible after install, surface finish and roundness are as much a selling point as cooling.

আবেদন: LED Bulbs and Retrofit Lamps
LED bulbs (A-shape, candle, reflector) and retrofit lamps use small aluminum discs spun or stamped into the heat sink base under the plastic or glass bulb.
The bulb’s driver and LED board sit on this aluminum body, which must shed heat into the ambient air. Because bulb heat sinks are small and thin, a high-conductivity 1050/1060 disc and good surface area (finned or fluted) are what keep a 5–15 W bulb running cool.
Retrofit compatibility adds constraints: the heat sink must fit the existing lamp envelope, be light, and not look like a block of metal. Spun and finned aluminum discs meet this, often with a glossy or anodized finish and a plastic skirt over part of the body.
The blank is small (50–120 mm) and thin, so consistency and burr control are critical for high-volume bulb lines.
Bulb heat sinks face a cost and size squeeze: the body must look like a classic bulb, keep the driver cool, and be cheap enough for a consumer lamp.
Spun and finned 1050/1060 aluminum does this, often with a plastic skirt over the middle and the aluminum fins exposed at the base.
Because these are made in the millions, disc diameter, gauge and edge must be rock-consistent so the spinning press does not jam or scrap.
Color and surface (রূপা, anodized black or painted) are cosmetic, but the underlying conductivity is what sets bulb life.

আবেদন: Street, High-Bay and Industrial Luminaires
Higher-power LED street lights, high-bay fixtures and floodlights move more heat and often use finned, machined or extruded aluminum rather than a simple spun cup.
The base plate starts as a thicker aluminum disc or plate—2–6 mm of 1050/1060, or stiffer 5052 for structural housings—and fins are machined or bonded to increase surface area.
The disc spreads heat from the LED array to the fins.
For these fixtures, thermal design is engineering-led: the base plate must be flat and thick enough to spread heat evenly across the array, and the surface must make good thermal contact with the LED board (often with thermal paste).
Outdoor use adds corrosion and weathering, so anodizing or coating is common. Here the disc is part of a engineered heat sink, not just a cosmetic cup.
High-power fixtures also demand good thermal contact between the LED array and the base plate. Warped or rough base plates create air gaps that act as insulation, defeating the best alloy.
A flat, পুরু 1050/1060 disc with a machined or sanded mounting face lets thermal paste fill the gap and spread heat to the fins.
Outdoor units further require anodizing or coating to resist humidity and road spray, so the disc surface must take that finish evenly and without blistering.

সারফেস ফিনিশ: অ্যানোডাইজিং, Blasting and Reflective Surfaces
The bare aluminum disc is often finished downstream. Anodizing grows a hard, protective oxide layer that improves corrosion resistance, gives electrical insulation (useful where the board mounts), and can be dyed black, silver or other colors.
Black anodizing also improves heat radiation from the surface. Sandblasting or texturing gives a uniform matte look; polishing or mirror finishing is used where the inner surface must reflect light.
Anodizing is the most common LED heat-sink finish because it protects the aluminum and adds the cosmetic black or white look of modern luminaires.
The blank itself should be clean and burr-free, because anodizing amplifies surface defects—scratches and rolling marks show up after anodizing rather than being hidden.
Reflective inner surfaces for PAR and spot reflectors may use bright or mirror-finish aluminum.
Because anodizing is a conversion of the surface rather than a paint, it follows the underlying finish: a smooth polished disc anodizes to a clean bright part, while a scuffed or rolled disc shows the marks through the anodic layer.
This is why heat-sink discs destined for anodizing are supplied with a clean, scratch-free surface and controlled rolling texture.
Black anodizing, বিশেষ করে, makes every surface flaw visible, so suppliers that know the lighting trade handle the discs carefully between blanking and delivery.

Thermal Design: How the Disc Cools the LED
Heat flows from the LED junction through the board and TIM (thermal interface material) into the aluminum disc, then conducts across the disc wall to the outer surface and radiates/convects to air.
The disc’s job is to spread heat from the small LED package over the whole heat-sink area. Three factors dominate: alloy conductivity (ব্যবহার 1050/1060), wall and base thickness (enough mass to spread heat), and outer surface area (পাখনা, fluting, black anodizing).
A common mistake is making the cup too thin to save weight: ক 0.4 mm wall may look fine but cannot spread heat, so the LED runs hot.
Thermal simulation or a simple temperature test (thermocouple on the junction, ambient and sink) validates the design. For high-power arrays, a thicker base plate and a properly sized disc diameter—rather than just a tall decorative shell—is what actually lowers junction temperature.
The interface between board and disc matters as much as the alloy. Even a 1050 plate fails if the LED board sits on it with air gaps or oxidation.
A flat, clean mounting face, thin thermal interface material, and good bolt pressure keep contact resistance low.
This is why machined base plates for COB modules are often specified with a flatness and surface finish callout rather than just a thickness.
The disc supplier controls flatness and gauge; the luminaire maker controls assembly pressure and TIM.
Quality Control of Heat-Sink Discs
| চেক করুন | প্রয়োজনীয়তা |
| খাদ / মেজাজ | মিল সার্টিফিকেট 1050/1060/1100 O or H |
| পুরুত্ব & ব্যাস | within tolerance, consistent across batch |
| সমতলতা | no wave or cupping; spins concentrically |
| প্রান্ত | burr-মুক্ত, no cracks or laminations |
| পৃষ্ঠতল | পরিষ্কার, তেল নেই, scratches or rolling defects |
| বিচার গঠন | sample spins/stamps without cracking or splitting |
| থার্মাল | conductivity per alloy (traceable via alloy cert) |
The converter trials a sample batch on its own spinning or stamping line before volume: if the disc cracks, spins eccentrically or leaves uneven wall thickness, খাদ, মেজাজ বা ফাঁকা ব্যাস বন্ধ.
Incoming checks of flatness, edge burr and gauge catch most problems; anodizing in-house further reveals surface defects that were invisible on the bare disc.
Custom Sizes and Tolerances
Heat-sink discs are cut to the customer’s blank size, not to a standard catalog.
The buyer provides the finished cup drawing or the spun dimensions, and the mill calculates the blank diameter, then cuts discs to that diameter in the required gauge and temper.
Because tooling for circle dies is low-cost, custom diameters are flexible; tight tolerances on diameter and flatness are specified for high-speed spinning.
For new luminaire designs, buyers often send the cup or base drawing and ask for a calculated blank size plus sample discs.
The converter spins or stamps the sample, adjusts the blank size if the wall thins unevenly, and then releases the specification for volume.
Hole patterns, centers or pre-punched features can be added for base plates, though most spun cups use a plain disc and form the features in the mandrel.
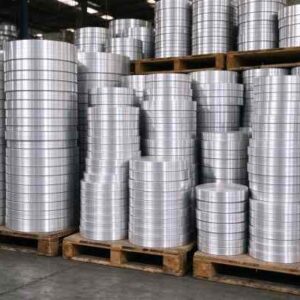
Because the discs are usually further formed or anodized, they are packed to stay clean and undamaged: stacked with interleaving paper to prevent scratches, banded on pallets, and wrapped against moisture and dust.
Anodizing-grade discs in particular must not be scuffed in transit, since every scratch shows after anodizing.
Export pallets are tagged with alloy, মেজাজ, ব্যাস, বেধ, lot and mill certificate, and shipped with the documentation the lighting maker needs for incoming inspection.

মূল্য এবং MOQ
Discs are priced on the aluminum base (LME-সংযুক্ত) প্লাস ফাঁকা এবং প্রক্রিয়াকরণ.
বিশুদ্ধ 1050/1060 discs cost a little more per kg than 3003 because of the rolling, but the thermal performance justifies it for heat sinks.
পুরুত্ব, ব্যাস, সহনশীলতা, cut quality and anodizing-ready surface affect price; পাতলা, বড়, tight-tolerance discs cost more than thick, loose ones.
MOQ is usually a few hundred kg or a pallet for custom sizes; standard sizes are quicker.
Buyers control cost by matching the alloy to the thermal job (not over-specifying to 5052 যখন 1050 is better), ordering container quantities, and getting the blank diameter right the first time—re-cutting because a cup splits wastes material and time.
মোট খরচ ফলন গঠন অন্তর্ভুক্ত: একটি ফ্ল্যাট, burr-মুক্ত 1050 disc with high yield beats a cheap disc that cracks on the spinning line.
How to Order LED Heatsink Discs
সংকর ধাতু বিবৃত কর (1050/1060/1100), মেজাজ (O for spinning, H for rigid plates) এবং বেধ.
Give the finished cup/base drawing or the blank diameter you need.
Specify diameter tolerance, সমতলতা, edge burr limit and surface condition.
Request a forming sample batch before volume production.
Confirm mill certificate for alloy and temper, and anodizing-ready surface if you anodize.
একটি ভালভাবে চালানো তদন্তের গতি বাড়ে. The buyer who sends the finished cup drawing (অথবা ফাঁকা আকার ইতিমধ্যে গণনা করা হয়েছে), লক্ষ্য পরিমাপক এবং মেজাজ, নিম্নধারার প্রক্রিয়া (স্পিনিং, stamping or CNC), and whether the discs will be anodized gets a quotation matched to the job rather than a generic per-kg price.
It also avoids the most common return—discs that are the wrong temper for spinning or that show scratches under anodizing.
চলমান উৎপাদনের জন্য, agree on a written spec sheet (খাদ, মেজাজ, গেজ, diameter tolerance, সমতলতা, প্রান্ত burr, পৃষ্ঠ, certificate) and reorder against it, so every shipment matches the approved sample.
Lead time is short for standard 1050/1060 discs in common sizes; custom diameters and anodizing-ready surface add a small setup.
Because aluminum pricing tracks the LME, quotations carry a short validity, so confirm price when the spec is locked.
ইকো প্রাক্তন সম্পর্কে
ইকো অ্যালাম মার্চ মাসে প্রতিষ্ঠিত একটি অ্যালুমিনিয়াম সরবরাহ বিশেষজ্ঞ 2025, বিশ্বব্যাপী গ্রাহকদের জন্য একটি যোগ্য চীনা অ্যালুমিনিয়াম রোলিং এবং ব্ল্যাঙ্কিং সাপ্লাই চেইন সমন্বয় করা.
আমরা প্লেটগুলিতে ফোকাস করি, কয়েল, ফয়েল, স্ট্রিপ এবং বৃত্ত জুড়ে 1000 সিরিজ (1050, 1060, 1070, 1100, 1235 এবং 1350), একসাথে 3003 এবং 5000-সিরিজ যেমন 5052.
বরং একক মিল ব্যবসায়ী, আমরা ডান মিল মেলে, খাদ, মেজাজ এবং প্রতিটি গ্রাহকের আবেদন কাটা এবং গুণমান পরিচালনা, শংসাপত্র এবং রপ্তানি প্যাকিং.
For LED lighting and heat-sink manufacturers, we supply high-purity 1050, 1060 এবং 1100 ও বা এইচ মেজাজে অ্যালুমিনিয়াম ডিস্ক এবং বৃত্ত, cut to spun-cup and base-plate diameters, ফ্ল্যাট সহ, burr-মুক্ত, anodizing-ready blanks and mill certificates.
আমরাও সরবরাহ করি 3003 এবং 5052 for stiffer formed or structural parts and 5052 reflective sheet where needed.
যোগাযোগ করুন [email protected] অথবা কল করুন +86 19924932491 with your cup drawing or blank size for a factory-coordinated quotation and forming samples.
We support lighting makers through the whole thermal-disc loop: blank-size calculation from your cup drawing, alloy and temper selection for spinning or CNC, ভলিউমের আগে নমুনা ডিস্ক, অনেক মিল সার্টিফিকেট, anodizing-ready surface handling, এবং সামঞ্জস্যপূর্ণ পুনর্বিন্যাস একই স্পেস ধরে.
বরং রিসেলিং, আমরা যোগ্য রোলিং এবং ব্ল্যাঙ্কিং মিলগুলির সমন্বয় করি যাতে ডিস্কগুলি সমতল হয়, burr-free and spin-ready—reducing the cracked cups and rejects that come from inconsistent or mis-specified stock.
প্রায়শই জিজ্ঞাসিত প্রশ্নাবলী
প্র: What aluminum disc is used for LED heatsinks?
ক: High-purity 1050, 1060 বা 1100 in O temper for spun cups and base plates; শক্তিশালী 3003/5052 only for structural or mechanically demanding parts.
প্র: Why not use a stronger alloy?
ক: Adding alloying elements (Mn, এমজি) raises strength but lowers thermal conductivity; a heat sink needs conduction more than strength.
প্র: O or H temper for spun LED cups?
ক: ও (নরম) for spinning and deep drawing; H14/H24 for shallow stamped pans and rigid base plates.
প্র: What disc thickness do I need?
ক: Spun cups about 0.6–2 mm; solid base plates for high-power LEDs about 2–6 mm, depending on thermal mass.
প্র: Can the discs be anodized?
ক: Yes—specify anodizing-ready, পরিষ্কার, burr-free blanks; anodizing gives protection, insulation and black/silver cosmetic finishes.
প্র: কিভাবে ফাঁকা ব্যাস গণনা করা হয়?
ক: From the finished cup’s surface area (drawing the spun shape), তারপর একটি গঠন নমুনা সঙ্গে বৈধ.
প্র: Are custom diameters available?
ক: হ্যাঁ - বৃত্ত কাটা কম টুলিং, so custom diameters and gauges are cut to your cup drawing.
প্র: How does the disc cool the LED?
ক: It spreads heat from the LED board through the aluminum wall to the outer finned or anodized surface, which radiates and convects to air.
উপসংহার
The aluminum disc is the thermal heart of most round LED luminaires.
High-purity 1050/1060/1100 in O temper gives the best balance of heat conduction and spinability, becoming the thin light cup of spotlights and downlights, the small body of LED bulbs, or the thick base plate of high-power fixtures.
ক্রয় পয়েন্ট সঠিক খাদ এবং মেজাজ হয়, গণনা করা ব্যাসের জন্য একটি সমতল বুর-মুক্ত ফাঁকা কাটা, anodizing-ready surface, এবং ভলিউম আগে একটি গঠন নমুনা.
একটি সমন্বিত সরবরাহ শৃঙ্খল থেকে সোর্সিং ডিস্ক যা খাদ নিয়ন্ত্রণ করে, মেজাজ, blanking and certificates gives lighting makers a consistent heat sink that spins cleanly, cools the LED reliably and looks good after anodizing.