
Aluminum Circle for Cookware | Deep Drawing Discs Factory
| Спецификация | Стойност |
| Сплав | 1050 / 1060 / 1100, 3003, 5052 |
| Темперамент | О (annealed for deep drawing) |
| Дебелина | 0.6–6 мм (pans 1.5–3 mm; heavy/induction 3–5 mm) |
| Диаметър | 100–500 mm, blanked to tooling |
| Induction | stainless clad base available / specified |
| Съответствие | FDA / ЕС 1935/2004 / LFGB food-contact as required |
| QC | alloy-temper certificate, дебелина, плоскост, draw-sample test |
| Основни продукти | уокс, frying pans, saucepans, stockpots, milk pans, тави за печене |
Aluminum Circle for Cookware
Въведение
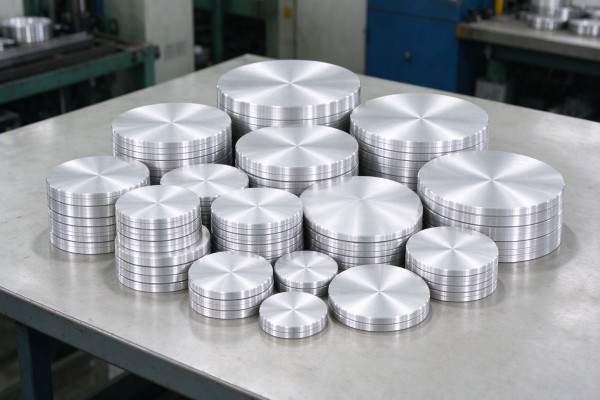
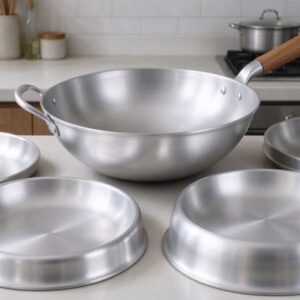
An aluminum circle for cookware is a round aluminum blank that is deep-drawn, spun or stamped into the body of a wok, frying pan, saucepan, stockpot, milk pan or baking tray.
It is the starting material for almost all pressed aluminum cookware: a flat disc is placed on a deep-drawing press and formed into a seamless cup, then trimmed, почистени, coated or anodized, and fitted with handles.
The quality of the circle directly determines whether the pan draws cleanly, holds an even wall, stays flat on the heat and takes a non-stick or anodized finish.
Cookware makers worldwide source these discs from Chinese aluminum mills because the rolling, blanking and deep-draw-ready supply is mature and cost-competitive.
This guide explains which alloys and tempers draw into cookware, the typical disc sizes for common pans, how deep drawing works and what causes earing, orange peel or cracking, how non-stick and anodized finishes and induction-clad bases are added, and how to specify and order consistent cookware circles.
It is written for pan factories, cookware brands and importers.
What Is an Aluminum Circle for Cookware?
The circle is a flat disc cut from aluminum coil or sheet, normally 0.6–6 mm thick and about 100–500 mm in diameter, supplied in the soft O temper so it can be formed.
Instead of buying a finished pan, the cookware factory buys the blank, draws it in its own tooling, then adds the interior coating, exterior finish, handles and packaging.
Supplying the circle rather than the finished body lets each factory control its own designs and branding.
Three properties make a circle good for cookware: it must be soft and ductile enough to deep-draw without cracking, it must have a clean, uniform surface so coatings adhere, and it must have low earing (uneven rim height) so little material is trimmed.
The right alloy, temper and annealing route all contribute, which is why not every aluminum sheet makes a good wok blank.
The most common cookware blanks are soft 1050 алуминиев кръг for pure-aluminum and economy pans, 3003 алуминиев кръг for general non-stick cookware, и 5000-серия алуминиев лист като например 5052 for premium hard-anodized bodies.
Circles are nested-blanked from coil at high speed, which is why they are an efficient starting part: the round blanks pack tightly across the strip, leaving little scrap, and the sheared edge is clean for the press.
Supplying a pre-blanked disc rather than a rectangular sheet also saves the cookware factory from running its own blanking line, so the factory can focus on drawing, coating and assembly.
The mill controls the annealing and the blanking tolerance, while the cookware factory controls its own tooling and finish.
Why Cookware Is Made From Aluminum Circles
-
- Висока термична проводимост: aluminum heats fast and spreads heat across the base, reducing hot spots.
- Ниска плътност: a deep-drawn aluminum pan is light and easy to handle, unlike cast iron or thick stainless.
- Отлична формиране: soft O-temper aluminum deep-draws into tall woks and pans in one or few presses.
- Surface-compatible: aluminum takes non-stick PTFE/ceramic coatings, hard anodizing and polishing well.
- Affordable: rolled and blanked circle material is low cost compared with cast, forged or stainless cookware.
- Рециклируеми: aluminum cookware is among the most recyclable kitchen products.
The main limitations are that bare aluminum reacts with acidic foods, which is solved by coating or anodizing; and that pure aluminum is not naturally magnetic, so induction cooktops require a bonded stainless steel base (covered in Section 11).
Compared with other cookware materials, aluminum sits between stainless steel and cast iron.
It heats faster and lighter than stainless, is far cheaper and more formable than copper, and does not carry the heavy weight or slow heating of cast iron.
That balance of speed, тегло, formability and cost is why the mass market—from consumer non-stick pans to commercial stockpots—is dominated by pressed aluminum drawn from circles.
A stainless pan is heavier and slower to heat, a cast iron pan is slow and heavy, and a copper pan is expensive; aluminum from a properly chosen circle gives the best everyday compromise.
Which Aluminum Alloy for Cookware?
| Сплав | Характеристики | Typical cookware use |
| 1050 / 1060 / 1100 | много мека, пластичен, good draw, ниска цена | pure-aluminum pans, milk pots, economy ware |
| 3003 (Ал-Мн) | умерена сила, good draw, здрав | general non-stick frying pans and saucepans |
| 5000 серия (5052) | по -силен, устойчиви на корозия, hard-anodizes well | premium hard-anodized cookware, heavy bases |
| 6061 / 6063 | heat-treatable, not the usual deep-draw blank | дръжки, капаци, структурни части |
Most pressed cookware uses 1050/1060 или 3003 in the O temper.
Pure 1000-series aluminum is the softest and cheapest and draws into simple pans and milk pots; 3003 adds manganese for a bit more strength and dent resistance, which is why it is the workhorse of non-stick frypans.
5052 is chosen when the pan must be thicker, heavier and hard-anodized, because the 5xxx film anodizes to a hard, durable dark surface. Buyers rarely need a 6xxx alloy for the drawn body; those grades are more often used for handles and lids.
For coated cookware the alloy matters less than the surface and temper, because the non-stick coating covers the aluminum.
For hard-anodized cookware the alloy matters a lot: 5052 огледален лист и 3003 anodize consistently, while very pure 1xxx gives a softer film.
The supplier should recommend the alloy once the factory says whether the pan will be non-stick, polished or hard-anodized.
Темперамент: Why O Is the Cookware Standard
Cookware circles are almost always supplied in the O (закален) темперамент.
O means the coil has been fully annealed, giving the lowest yield strength and the highest elongation, which is exactly what deep drawing needs: the metal flows into the die without tearing.
A work-hardened H temper circle would crack or wrinkle when drawn into a deep wok, and a half-hard disc would spring back.
So even when the finished pan feels rigid, the blank arrived soft.
The anneal must be correct: too soft and the blank wrinkles or thins unevenly; too hard and it cracks at the corner.
A consistent, low-earing O-temper circle from a hot-rolled, well-annealed coil gives the most stable deep drawing.
For very shallow parts some factories use a light H12/H14 temper, but deep woks, deep saucepans and tall stockpot bodies always use O.
The annealing route also sets the grain size and texture. A coil annealed to a fine, uniform grain draws smoothly and shows little orange peel, while an over-annealed or coarse-grain coil gives a textured surface on the bright pan.
The rolling direction and the subsequent anneal control earing: a well-processed hot-rolled circle draws with almost no lobes, so the trim scrap is low and the press runs cleanly.
This is why cookware buyers ask for the annealing practice, not just the temper letter, when qualifying a new mill.
Typical Dimensions and Pan Sizes
| Параметър | Типичен диапазон | Бележки |
| Дебелина | 0.6–6 мм | pans 1.5–3 mm; heavy/induction bases 3–5 mm |
| Диаметър | 100–500 mm | sized to the drawn pan and trimming allowance |
| Темперамент | О | annealed for deep drawing |
| Плоскост | no buckle or wave | must lie flat in the die |
| Ръб | clean bur-free shear | no sharp burr that marks the die |
The circle diameter is larger than the finished pan because deep drawing consumes material around the rim that is later trimmed off.
А 280 mm frying pan typically starts from a blank around 450–550 mm depending on the depth; tall woks and deep stockpots need a much larger blank than a shallow skillet.
The cookware factory calculates the blank size from its draw, and the mill blanks to that exact diameter with a dedicated die.
Tolerances are tight because the blank must nest in the die and draw evenly.
Thickness varies only a few hundredths of a millimeter across the coil, diameter is held to the blanking die, and the disc must be flat and free of waves; a buckled circle wrinkles in the press.
The sheared edge is also clean and deburred so it does not mark the die or create a sharp rim on the finished pan.
These controls are what separate a cookware-grade circle from general aluminum sheet.
A typical illustration: a 280 mm диаметър, 50 mm deep skillet might start from a blank around 480 мм, while a 320 mm wok 100 mm deep may need a 600 mm blank.
The extra diameter is material pulled down the wall and trimmed off the rim, so a deep pan consumes far more blank than a shallow one.
Weight and thickness are checked against the part: a heavy commercial stockpot uses a 4 mm circle, while a light consumer frypan uses a 1.8–2.5 mm circle.
The cookware factory shares its draw, and the mill confirms the blank diameter and thickness before tooling.
How a Circle Becomes a Pan: Дълбоко рисуване
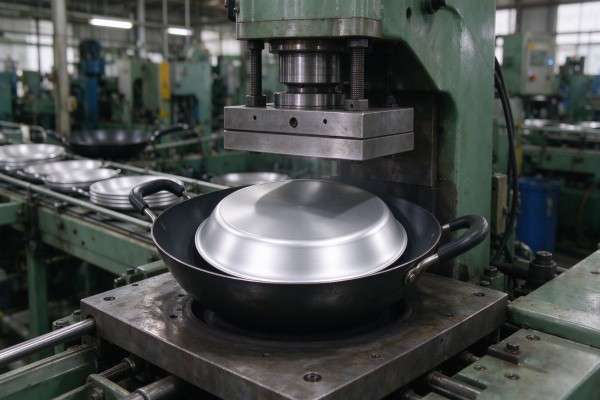
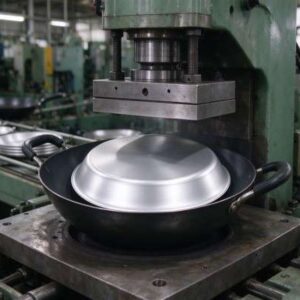
Deep drawing places the flat circle over a die cavity, holds it down with a blank holder to control wrinkling, and pushes a punch into the disc so the material flows downward into a cup.
In one stroke the flat blank becomes a seamless pan body; taller or deeper parts use multiple draws, with an intermediate anneal if the work hardens.
The blank holder force, lubrication and punch/die clearance are tuned so the wall thins evenly and the corner does not tear.
The limiting draw ratio (LDR) describes how deep a cup can be pulled from a given blank before tearing: мек О-нрав 1050/3003 draws deeper than hard-temper or higher-strength alloys.
Thin pans are drawn with a relatively thick blank and trimmed; heavy commercial stockpots use a thick circle and sometimes ironing (wall-thinning) after drawing to make a tall, straight-sided pot.
Consistent circle thickness and low earing are what let the press run at high speed without line stops.
Very deep or straight-sided parts are often made in more than one draw: a first shallow cup is redrawn through a smaller die to increase depth, and if the wall must be thinned for a light, tall pot, an ironing step squeezes the wall between punch and die.
Each draw work-hardens the aluminum, so intermediate annealing restores ductility between operations.
A consistent circle—same thickness, same temper, same grain—is essential across these steps, because a variation in the blank changes the draw and can tear at the corner.
Drawing needs three things tuned together: enough blank-holder pressure to stop the flange wrinkling, the right die/punch clearance so the wall thins rather than folds, and press lubrication that lets the aluminum slide over the tool without galling.
Too little hold-down wrinkles the rim; too much cracks the corner. A soft, consistent O-temper circle responds predictably to these settings, which is why a stable blank lets the press run fast with few rejected parts.
Common Drawing Defects and Their Cause
| Дефект | Външен вид | Main cause |
| Обеци | wavy lobes on the drawn rim | uneven crystallographic texture / poor anneal |
| Orange peel | rough grainy surface | coarse grain in the blank |
| Strain lines / разкъсване | cracks or lines at the corner | too hard temper, too deep a draw, poor clearance |
| Wrinkling | waves on the wall or flange | blank holder too light or blank too thin |
| Uneven wall | thin spot that burns through | poor lubrication or uneven thickness |
Earing is the most circle-specific defect: it shows as four or six lobes around the rim after drawing, forcing extra trimming and scrap.
It comes from the way the coil was rolled and annealed, so a low-earing, hot-rolled O-temper circle is essential for high-volume pans.
Orange peel comes from a coarse grain and shows as a textured surface on the finished pan, which is visible on polished or bright surfaces.
Cracks and tearing usually mean the temper is too hard for that draw depth, or the die clearance and lubrication are wrong.
A cookware factory should run a draw trial with the first lot to confirm the circle behaves in its die.
Most of these defects are avoided upstream, not in the press.
Earing and orange peel are set by the coil’s rolling and annealing route, so a low-earing, fine-grain, hot-rolled O-temper circle prevents them before stamping; cracking is prevented by supplying the correct soft temper for the draw depth; wrinkling by the correct blank-holder pressure; and coating blemishes by clean, oil-free material.
This is why a cookware factory qualifies a mill with a draw sample rather than buying on price alone, and why repeat orders stay on the same coil specification.
Cookware Made From Circles
The same blanking and deep-drawing route produces most pressed aluminum cookware.
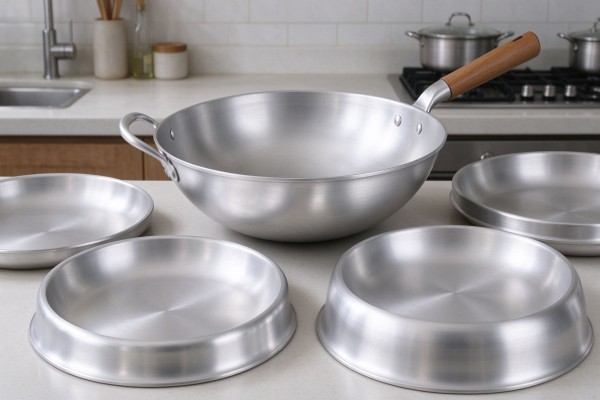
Frying pans and skillets are shallow draws from a thin circle; woks are deep draws that need a very ductile O-temper blank; saucepans and stockpots are deeper, straight-sided draws, often with a heavier base; milk pans and baking trays are shallow, simple forms.
Commercial kitchen stockpots use thick, robust circles, while consumer non-stick pans use thinner, lighter ones.
After drawing, the body is trimmed to a clean rim, the edge is curled or rolled, handle holes are punched, the surface is treated, and the interior is coated or polished.
Handles and lids are then riveted or screwed on. Because the drawn body is seamless, there is no welded corner to leak or trap food, which is why pressed aluminum cookware is easy to clean.
Consumer and commercial cookware differ in the circle they draw.
Household non-stick pans use thin 1.5–2.5 mm O-temper 1050/3003 circles for lightness and low cost; restaurant stockpots and woks use thick 3–5 mm 3003 или 5052 circles that stand up to daily heavy use, denting and alkaline cleaning.
Premium consumer hard-anodized sets sit between the two, using a mid-thick 5052 body that anodizes to a durable dark surface. The same drawing line can serve both markets by changing the alloy, gauge and finish.
Surface and Coating After Drawing
The drawn aluminum body is finished in one of several ways.
Most consumer non-stick pans are degreased, then grit-blasted or chemically etched to give the coating a grip, sprayed with a primer and one or more PTFE (Teflon-type) or ceramic non-stick layers, and cured in an oven.
Premium pans are hard-anodized to a thick, dark, non-reactive oxide layer, sometimes with a non-stick coating over it; economy and commercial pans are left polished or satin.
The cleanliness and grain of the original circle matter here, because any scratch or rolling mark shows through a coating.
Non-stick lines coat dozens of bodies per hour on a conveyor, so the incoming drawn bodies must be consistent in size and surface.
A circle with a dirty or oxidized surface gives poor coating adhesion; a circle with orange peel gives a textured interior.
This is why cookware makers ask their mill for a clean, закален, low-contamination O-temper disc rather than the cheapest possible scrap-tainted sheet.
The three finishes suit different price points. PTFE non-stick is the most common, durable and affordable, sprayed in multiple primer-and-topcoat layers and cured;
ceramic non-stick is a newer, inorganic option marketed as free of PTFE, with different wear behavior; and hard anodizing builds a thick, dark, non-reactive oxide that can stand alone or carry a non-stick coat.
All three depend on a clean, properly prepared aluminum surface—oily, oxidized or orange-peel material ruins adhesion—so the incoming circle quality is as important as the coating line itself.
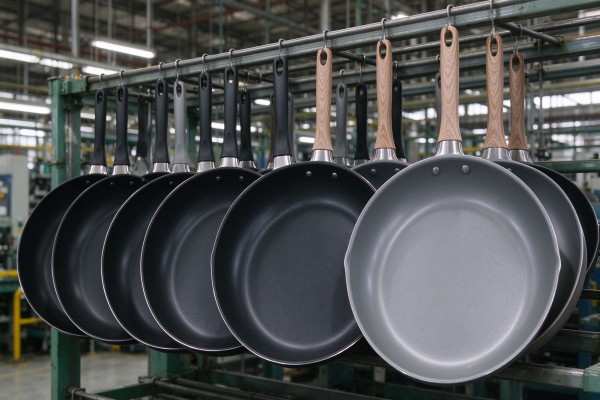
A typical non-stick line degreases and etches the drawn body, applies a primer that bonds to the aluminum, then one or two topcoat layers, and cures each in an oven.
Film build, cure temperature and cleanliness control how long the coating lasts.
Because the coating is thin, any deep scratch, orange-peel grain or oily residue on the incoming blank shows through, which is why a clean, fine-grain circle is the silent requirement of a good non-stick factory.
Induction and Clad Bases
Aluminum is not magnetic, so a bare aluminum pan will not heat on an induction hob.
The standard solution is to bond a magnetic stainless steel disc (обикновено 430 или 304) to the bottom of the drawn body.
This is done by inserting a stainless sheet between the aluminum circle and a lower aluminum layer before drawing, or by bonding/stir-welding a stainless disc to the finished base and then flattening it.
The result is a clad base: an aluminum core inside for fast, even heat, a stainless layer outside that induction heats, and a flat, stable bottom.
Clad cookware needs a slightly thicker, sturdier circle and a precise bonding operation.
The base must stay perfectly flat after bonding and heating, or the pan rocks on the hob and hot spots form.
For induction lines the cookware factory should specify the base thickness and stainless type, and the mill should supply a circle flat and thick enough to support a clad base without warping.
Two common routes make the clad base.
In the more expensive route a stainless sheet is sandwiched under the aluminum circle before drawing, so the base is bonded through the forming heat; in the common route a stainless disc is bonded or friction-stir welded to the finished pan bottom and then re-flattened.
The bond must be void-free so heat transfers evenly, and the final base must be dead flat or the pan rocks on the glass hob.
A warped base is a frequent complaint, which is why a thick, плосък, dimensionally stable circle matters for induction ware.
Food-Contact Compliance
Because cookware touches food, the aluminum and any coating must comply with food-contact regulations in the destination market.
The common benchmarks are the US FDA aluminum and coating requirements, the EU Framework Regulation (ЕК) 1935/2004 and German LFGB, which include migration tests.
Non-stick coatings must themselves be food-safe, and hard-anodized cookware must be properly sealed.
The supplier should provide mill certificates and, където се изисква, food-contact declarations for the alloy and the finish rather than a generic claim.
Bare aluminum cookware is suitable for most foods, but acidic foods (домати, wine, цитруси) can react, which is why those pans are almost always coated or anodized.
Buyers should ask for the specific migration or food-contact report for the market they sell into, and keep the lot number with the goods so a product can be traced back to the coil.
На практика, the documents a cookware brand should request are: a mill test certificate naming alloy and temper, a food-contact or migration declaration for the aluminum (and for non-stick pans, the coating’s own food-safe approval), and—where the market requires it—LFGB or EU migration results.
A generic statement that the material is “food-grade” without a test report is not enough for a regulated brand.
Hard-anodized cookware must also show that the anodic film is properly sealed, because an unsealed oxide can take up flavor or color.
Quality Control of Cookware Circles
| Check | Типично изискване | Метод |
| Сплав / темперамент | 1050/3003/5052 in O temper | сертификат за мелница, hardness test |
| Дебелина | per drawing, tight tolerance | micrometer on samples |
| Диаметър | per blanking die | caliper / sample check |
| Плоскост | no buckle or wave | visual and flat-bed inspection |
| Повърхност | no oil, драскотини, следи от преобръщане | visual before drawing |
| Drawing trial | no crack, low earing | first-article draw test |
| Адхезия на покритието | no peel after cure | cross-hatch / abrasion test |
For a new pan tooling, a first-article draw trial is the most valuable check: a sample lot is drawn in the factory’s press to confirm the circle cracks, ears or thins before a full container is committed.
Once a lot is proven, repeat orders run on the same coil spec, anneal and die, which keeps the draw consistent. Incoming inspection verifies the certificate alloy, темперамент, thickness and diameter, and rejects oily or scratched material that would ruin the coating.
Because the circle is soft, handling marks are easy to create and easy to miss.
A qualified lot is sampled across the pallet, not just from the top, because edge dents, corrosion spots and interleaf contamination can hide in the middle of a stack.
For coated lines, a cross-hatch adhesion test after cure quickly reveals whether the incoming surface was clean enough.
Keeping the approved draw sample and a coated first article lets the factory compare every repeat shipment visually.
Packaging and Logistics
Circles are flat and scratch-sensitive, so they are stacked in clean cartons or on fumigated pallets, often with interleaving paper between faces to prevent rubbing and scratches, and edge-protected.
Because any scratch on the face shows through a coating, handling is kept clean and dry.
Each carton is tagged with alloy, темперамент, дебелина, диаметър, coil/lot number and weight.
Export terms are commonly FOB, CFR or CIF with 30% T/T deposit and balance against the bill of lading, with the mill certificate and food-contact documents shipped with the goods.
Material should be stored dry and flat; stacked circles can develop a set or buckle if left unevenly loaded.
Because the blank is soft O-temper, dents from rough handling are visible on the finished pan, so pallets are strapped and edge-protected for export.
Because O-temper aluminum is soft, large stacks should not be over-packed or left under uneven pressure, or the bottom discs develop a permanent set that will not lie flat in the die.
Cartons are usually weighed and counted, and the coil/lot number is kept on the outside so the cookware factory can trace a drawn pan back to the exact coil if a quality issue appears.
Interleaving paper also stops the faces rubbing together during a long sea voyage.
Pricing and MOQ
| Cost factor | Effect on price |
| Сплав | 1050/1060 най-нисък; 3003 mid; 5052 по-високо |
| Темперамент / route | low-earing hot-rolled O-temper draws better and costs a little more |
| Дебелина | thicker heavy-gauge circles cost more |
| Диаметър / tooling | custom diameter needs a blanking die (one-time) |
| Повърхност | чиста, low-defect material for coating adds consistency |
| Обем | container runs and standard gauges lower the unit cost |
Circle price follows the aluminum ingot base (LME and Shanghai spot) plus rolling, отгряване, blanking and a small premium for cookware-grade consistency.
Custom diameters carry a one-time blanking die, which is amortized over the order; using an existing diameter or a common size removes it.
The lowest-cost scrap or off-temper material is usually a false economy, because a cracked or earing lot stops the coating line.
A small first sample lot is recommended before a full container.
Because the ingot base floats, quotes carry a short validity and are re-confirmed when the order is placed; large metal moves shift the per-disc price noticeably.
Buyers control cost by fixing the alloy and gauge across a product family, choosing an existing blank diameter where possible, ordering full containers, and not over-specifying a thicker circle or a higher alloy than the pan needs.
А 5052 circle costs more than 3003, but it is only worth it where hard anodizing or heavy commercial use demands it.
How to Order Cookware Circles
Send the pan drawing or the finished size, depth and wall so the blank diameter can be calculated.
State the alloy (1050/3003/5052), O Темпер, thickness and the finish (non-stick, анодизиран, полиран).
For induction pans, specify the clad base thickness and stainless type.
Approve a sample draw lot, confirm earing, surface and coating adhesion.
Confirm price, die tooling, MOQ, packaging and delivery terms, then run production with full certificates.
For a first order, a short sample lot pays for itself. It confirms that the circle draws cleanly in your specific die, that earing and orange peel are acceptable, and that the coating or anodizing adheres before a full container is committed.
Once approved, the mill holds the blanking die and records the coil spec, anneal and thickness so repeat orders match the approved sample.
Sharing your die draw and any existing problem—tearing, обеца на ухото, coating peel—helps the supplier tune the material rather than guess.
За еко алумия
Eco Alum is an aluminum product supplier established in March 2025, organized around a rich supply chain within China’s aluminum rolling industry.
Instead of acting as a simple trader, we coordinate with qualified rolling, blanking and deep-draw-ready mills to deliver specification-accurate, well-finished material at factory-direct pricing and manage the technical, quality and export documentation.
Our main products are aluminum plates, бобини, фолиа, strips and discs (circles), covering the 1xxx series—1050, 1060, 1070, 1100, 1235 and 1350—along with 3003 and the 5000-series alloys such as 5052.
For cookware we supply O-temper deep-drawing circles in 1050/1060, 3003 и 5052, to your diameter and thickness, with low earing, clean coating-ready surfaces, mill certificates, food-contact documents where required, and scratch-proof packing.
We help calculate the blank size for your pan, recommend the alloy for non-stick, hard-anodized or induction-clad cookware, and support a draw-sample before volume production.
Reach us at [email protected] or +86 19924932491.
We support pan factories and cookware brands with blank-size guidance, low-earing O-temper material, lot-specific mill and food-contact certificates, постоянна дебелина, и чисти, interleaved packing.
Send your pan drawing or required diameter to [email protected] for a prompt, specification-based quotation and draw samples.
We support the whole sourcing loop rather than just shipping discs: blank-size calculation from your pan drawing, alloy and temper selection for non-stick,
hard-anodized or induction use, draw-sample approval before volume, lot-specific mill and food-contact documents, and consistent reorders held to the same coil spec.
Because we coordinate with qualified rolling and blanking mills, the circles arrive clean, soft and low-earing, ready for your deep-drawing press.
Често задавани въпроси
Q: What aluminum circle is used for cookware?
А: Most pressed cookware uses soft O-temper 1050/1060 или 3003 circles; premium hard-anodized pans use 5052.
Q: Why must the circle be in the O temper?
А: O is the fully annealed, softest condition, which deep-draws into woks and pans without cracking or springback.
Q: How is the blank size calculated?
А: It is larger than the finished pan because deep drawing trims the rim; the cookware factory calculates it from the pan depth, and we blank to that diameter.
Q: Why do my drawn pans show wavy edges?
А: That is earing, caused by uneven coil texture. A low-earing, properly annealed hot-rolled circle reduces it.
Q: Can aluminum cookware work on induction?
А: да, by bonding a magnetic stainless steel disc (clad base) to the bottom of the drawn aluminum body.
Q: Is aluminum cookware food-safe?
А: да, when it meets FDA, ЕС 1935/2004 or LFGB food-contact rules; acidic foods are best in coated or anodized pans.
Q: What thickness circle do frying pans use?
А: Common pan bodies are about 1.5–3 mm; heavy commercial stockpots and induction-clad bases run 3–5 mm.
Q: Can you supply draw samples before a full order?
А: да. A small sample lot lets the factory trial its die, confirm earing and coating adhesion, and approve the material.
Заключение
Накратко: for everyday non-stick consumer pans, мек О-нрав 1050/1060 или 3003 circles are the standard; for hard-anodized premium cookware, използване 5052 или 3003; for commercial stockpots and induction-clad bases, use a thicker, sturdier 3003/5052 кръг.
Specify O temper, low earing, clean surface and a flat, tight-tolerance disc, and approve a draw sample before volume.
With the right circle, the press runs cleanly, the coating adheres, and the finished pan is flat, smooth and durable.
The aluminum circle is the heart of pressed cookware. A clean, мека, low-earing, О-нрав 1050, 3003 или 5052 circle deep-draws into woks, frying pans, saucepans and stockpots, takes a non-stick or hard-anodized finish, and can be clad for induction.
The specification follows the product: pure aluminum or 3003 for everyday non-stick pans, 5052 for premium hard-anodized bodies, thicker blanks for commercial and induction ware, and a low-earing, coating-ready surface for consistent output.
Sourcing from a supplier that understands deep drawing, blank size and food-contact compliance—and that approves a draw sample before volume—gives cookware makers a circle that runs cleanly in the press and finishes to a flat, гладка, durable pan.