


1060 Aluminum Circle Manufacturers

| Špecifikácia | Hodnota |
| Product name | 1060 Hliníkový kruh (Aluminum Disc / Round Blank) |
| Zliatina | 1060, Al ≥ 99.60% |
| Temper | O (mäkké, hlboká kresba); H12 / H14 / H22 / H24 |
| Casting route | hot-rolled (DC, low earing) or twin-roll cast |
| Hrúbka | 0.2– 6 mm (cookware commonly 0.5–4 mm) |
| Priemer | 80– 1200 mm (cut to tooling) |
| Tolerancie | thickness ±0.02 mm; diameter ±1.0 mm |
| Limiting draw ratio | about 1.8–2.0 (1060-O) |
| Štandardné | GB/T 3880, ASTM B209, IN 485 |
| Povrch / okraj | mill, leštený, kefovaný, eloxované; deburred, byt |
| Main applications | riad, reflektory svietidiel, znaky, plechovka & hardvér |
| Certifikát | MTC EN 10204 3.1; ISO 9001; FDA/LFGB/RoHS as relevant |
| Moq / dodacia lehota | trial lot or container; lead time by tooling and quantity |
| Balenie / terms | interleave, pallet, moisture-proof export; FOB/CFR/CIF |
1060 Aluminum Circle Manufacturers
Zavedenie
1060 aluminum circles are round, ready-to-form discs blanked from high-purity aluminum coil.
They are the standard starting blank for deep-drawn and spun cookware—non-stick pans, pressure cookers, stock pots and kettles—and are also drawn or spun into lamp reflectors, dopravné značky, menové štítky, battery and capacitor cans and many other stamped parts.
For a converter or cookware factory, the blank is where product quality begins: a circle that is the right gauge, miernosť, byt, burr-free and low in earing will form efficiently on a press line; a poor one causes cracked walls, uneven rims and coating defects that cost far more than the metal itself.
That is why choosing among 1060 aluminum circle manufacturers matters as much as the alloy.
The name 1060 only defines the chemistry; real performance is decided by how the coil was cast, rolled, annealed and blanked, and by how tightly the supplier controls gauge, surface and lot consistency. Táto príručka sa týka zliatiny, veľkosti, výroba, the main applications (with cookware in the most detail), quality and standards, pricing, ordering, and a core specification table.

What Is a 1060 Hliníkový kruh?
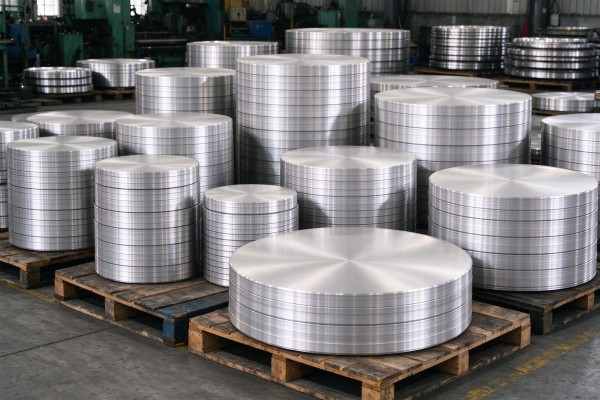
A 1060 aluminum circle—also called an aluminum disc, round blank or wafer—is a flat circular piece cut from 1060 cievka. It is a semi-finished product: buyers do not use it flat but form it in a press, drawing die or spinning lathe into a three-dimensional part. The disc is made to the exact diameter and thickness the customer’s tooling requires.
1060 is a commercially pure 1xxx aluminum with a minimum aluminum content of 99.60%, non-heat-treatable and strengthened only by cold work or softened by annealing. In the soft O condition it has low yield strength and high elongation (often 30–40% or more), so it draws and spins without cracking.
It also offers high thermal conductivity (o 234 W/m·K), good corrosion resistance and a surface that polishes, anodizes and coats well. Its controlled impurities are:
| Prvok | A | Fe | Cu | Mn | Mg | Zn | z | Al |
| 1060 limit | ≤0,25 | ≤0,35 | ≤0,05 | ≤0,03 | ≤0,03 | ≤0,05 | ≤0,03 | ≥99,60 |
The trade-off is strength: 1060-O is soft (tensile roughly 60–100 MPa), which is ideal for a saucepan or shade but not for load-bearing or pressure parts, kde 3003 alebo 5052 is correct.
Circles are the circular, press-ready form of the same 1060 coil used for flat products, blanked from the identical material used for the 1060 hliníkový plech and coil, so chemistry, surface and certification are continuous across both shapes.
Buying ready circles rather than blanking coil in-house suits most converters: the circle mill runs high-yield servo blanking lines and reuses the skeleton, so it absorbs the scrap and tooling cost, while the converter avoids running a blanking press, stocking wide coil and managing edge scrap.
The trade-off is that the diameter and temper must be specified accurately for each tool set; once that is fixed and a sample is signed, circle supply is repeatable and low-touch.
1060 vs Other Aluminum Circle Alloys
1060 is not always the best choice. The correct alloy depends on draw depth, required stiffness, surface and cost.
| Zliatina | Čistota / key element | Formovanie / silu | Typical circle uses |
| 1050 | Al ≥99.50% | veľmi mäkké, tvárny; weakest | svetelné reflektory, značky, cheap spinnings |
| 1060 | Al ≥99.60% | excellent deep drawing; vyvážený | most cookware, lampy, znaky, hardvér |
| 1100 | Al ≥99.00%, small Cu | slightly stronger, tvárny | chemical ware, general spinnings |
| 3003 | Al + 1.0-1,5 % Mn | ~15–20% stronger, good draw | hard-wearing pans, pressure cooker, battery cans |
| 3004 / 5052 | Mn+Mg / ~2.5% Mg | vyššia pevnosť | deep cans, pressure and industrial parts |
1060 is the market default for cookware: purer and better-drawing than 1100, slightly stronger than 1050. For very light or cost-sensitive reflectors some buyers use a
1050 hliníkový kruh. For pressure cookers, hard-wearing pans and power-battery cans a 3003 hliníkový kruh je silnejší; clad or induction bases often combine a 3003 hliníková cievka core with a magnetic stainless skin. A good supplier recommends the alloy from the part design rather than confirming 1060 for everything.
A simple decision rule keeps the choice clear: for a deep-drawn or spun cookware body or reflector with no high load, 1060-O is the default; for the cheapest, softest reflector or a very light tag, 1050 can lower cost; for abrasion, pressure or a rigid rim, move to 3003 a, for the most demanding cans, 3004 alebo 5052.
Forming difficulty is the other lever—the taller and thinner the draw, the more value there is in low-earing hot-rolled O stock rather than the cheapest cast-rolled coil. Giving the mill a sample part, its draw depth and the downstream coating lets it recommend both alloy and casting route.
Špecifikácie, Sizes and Tempers
| Parameter | Typický rozsah pre 1060 kruhy |
| Zliatina / štandardné | 1060, Al ≥ 99.60% (GB/T 3880 / ASTM B209 / IN 485) |
| Temper | O (hlboká kresba); H12/H14/H22/H24 (firmer); H16/H18 on request |
| Hrúbka | about 0.2–6 mm (cookware commonly 0.5–4 mm) |
| Priemer | about 80–1200 mm (cut to tooling) |
| Tolerancie | thickness often ±0.02 mm; diameter ±1.0 mm |
| Povrch / okraj | mill, leštený, brushed or anodized; blanked, deburred, byt |
The cookware sweet spot is 0.5–3 mm and 100–400 mm; large pots and pizza trays run to 400–600 mm, and industrial spinnings or vessel heads to 800–1200 mm.
The soft O temper gives the highest draw ratio and is the cookware standard; H12/H14/H22/H24 suit shallow forms, signs and stiffer spinnings. Edge and flatness matter for automatic feeding, and the face must be clean and oil-free for later anodizing or coating.
Choosing the temper is the first practical decision: O is the default for any deep draw, while H12/H14 and H22/H24 add stiffness and dent resistance for shallow stampings and signs at the cost of ductility.
An order is fully defined by five parameters—alloy, miernosť, hrúbka, diameter and surface—plus tolerance, okrajový stav, packing and the target standard. Supplying the actual drawing or a sample disc removes ambiguity, especially for imperial gauges such as 0.050 v / 1.27 mm.
Weight follows the aluminum rule: hmotnosť (g) = π × (radius in m)² × thickness (mm) × 2.71 × 1000 (hustota 2.71 g/cm³). A 2.0 × 320 mm disc weighs about 0.436 kg. Because circles are cut from rectangular coil, the nesting layout and scrap percentage are the key cost driver.
Ako 1060 Circles Are Made
Circle quality is decided before blanking. Two routes produce the coil. In direct-chill (DC) casting plus hot rolling, molten metal is cast into an ingot, homogenized and hot-rolled into a symmetric, low-anisotropy band that draws with the least earing—preferred for tall, one-piece cookware and pressure vessels.
In twin-roll continuous casting, molten metal solidifies directly between chilled rolls into a thin strip; it is faster and cheaper for shallow and medium parts but can show higher earing unless rolling and annealing are carefully designed. A transparent mill states the route.
The strip is then cold rolled to the final gauge, setting thickness accuracy and surface. For O-temper circles the coil is annealed in a controlled-atmosphere furnace to recrystallize the grain: under-annealing leaves it hard and low in elongation, over-annealing creates a coarse grain that gives orange peel after drawing.
Finally the coil is leveled, de-greased and fed into an automatic blanking line, where a hardened multi-cavity die punches the circles. Staggered or zigzag nesting lifts material utilization into the high 70s to mid-80% range, directly cutting per-piece cost. Discs are deburred, leveled, inspected, interleaved and moisture-proof packed.
Nesting is the key cost lever: the circles are cut from a rectangular coil and the skeleton between them is worth only scrap value, so the layout—square, staggered or zigzag rows, often on swing-blanking lines that also recover the edge into smaller discs—sets utilization.
Every percentage point of yield is a direct per-piece saving, which is why a mill that blanks its own coil undercuts resellers buying pre-blanked discs.
The edge matters too: a cleanly sheared, deburred, flat edge lets discs stack and feed without jamming on high-speed presses and stops a burr from transferring a mark into the drawn wall.

Základná aplikácia: Cookware and Kitchenware
Cookware is the largest and most demanding application. Aluminum conducts heat roughly four to five times faster than stainless steel and spreads it across the base, while the soft O disc can be drawn into a seamless deep vessel in one or a few operations.
| Cookware product | Typical circle | Formovanie / zakončiť |
| Non-stick frying pan / skillet | 0.5–3 mm, Ø100–400 | single draw + PTFE/ceramic |
| Pressure cooker / heavy base | 2–4 mm | multi-draw; 3003/3004 voliteľný |
| Stock pot / saucepan | 1–3 mm | single or multi draw |
| Kettle / coffee pot | 0.6–1.5 mm | hlboká kresba + pradenie |
| Pizza pan / baking tray | 0.6–2 mm | plytké kreslenie + anodize |
| Rice-cooker inner pot | 1–2.5 mm | hĺbka + induction base |
6.1 Deep drawing and spinning
Deep drawing pulls the disc over a punch and into a die to form a cup. The limiting draw ratio (blank diameter over punch diameter) is about 1.8–2.0 for good 1060-O; deeper parts need multiple draws, sometimes with an intermediate anneal. The blank-holder force is the central control: too high splits the wall at the punch radius, too low causes wrinkling.
Earing—the uneven rim peaks caused by the coil texture—is the most visible defect, and good cookware stock targets a low earing value, often around 4% alebo menej, so the rim trims flat. Spinning forms a rotating disc over a mandrel into curved or parabolic kettles, woks and reflectors using low-cost tooling.
In a first draw the blank holder grips the flange while the punch pushes the center into the cavity; the flange metal flows inward and the wall thins, especially near the punch radius. Drawing lubrication, a polished die and generous radii keep the flow even and avoid galling.
When the required depth exceeds the single-draw ratio, the part is redrawn at a smaller diameter, with an intermediate anneal restoring ductility if the metal work-hardens.
The starting disc is sized to the area of the finished cup plus the trimmed rim, so blank diameter and thickness are set together. A low-earing, hot-rolled O blank with the right texture is what allows a tall, one-piece pot to form in one stroke without trimming a wavy rim.
6.2 Surface finishing and the right alloy
Po formovaní, pans are sandblasted or de-greased and coated with PTFE (now commonly PFOA-free) or ceramic, hard-anodized, or bright-finished.
Each route assumes a clean, bez oleja, pinhole-free blank. 1060 is the economical, easy-to-coat body; pressure cookers and induction-ready pans use 3003 or a clad disc, and the supplier should recommend the alloy from the pan design rather than apply one universally.
6.3 Surface finishing in detail
Mechanical preparation comes first: polishing gives a reflective face, brushing a satin hairline that hides minor marks, and sandblasting a uniform matte key that helps non-stick coating adhere.
Anodizing converts the surface into a controlled oxide layer—roughly 5–15 µm in standard sulfuric anodizing, thicker and denser in hard anodizing—that is hard, odolný voči korózii, colorable and non-peeling; bright or mirror anodizing maximizes the reflectivity of lamp shades.
Non-stick cookware uses a primer plus one or more PTFE (commonly PFOA-free) or ceramic top coats cured at high temperature, while signs and hardware use powder or polyester color coating.
Pre-coated circles can be supplied for shallow forms, but severe deep draws are coated after forming because the film would otherwise tear. Every route assumes a clean, bez oleja, pinhole-free blank with a fine, uniform grain.
6.4 How aluminum compares with other cookware materials
Aluminum is the best heat conductor of the common cookware metals, warming quickly and spreading heat across the base to reduce hot spots, while staying light and drawing readily into deep, seamless bodies. Its limits are softness and a non-magnetic surface, so it is anodized or coated and uses a clad magnetic base for induction. The comparison below summarizes the trade-offs.
| Materiál | Heat spread | Váha | Key notes |
| 1060 / 3003 hliník | vynikajúce, fast and even | svetlo | hlboko ťahané, coated or anodized; clad base for induction |
| Nehrdzavejúca oceľ | poor and uneven alone | stredná | trvanlivé, non-reactive; bonded to an aluminum core |
| Uhlíková oceľ | dobre | light-medium | thin and responsive; rusts without seasoning |
| Cast iron | slow, high heat capacity | ťažký | holds heat; too heavy and slow for light drawn ware |
| Multi-layer clad | vynikajúce | medium-heavy | aluminum core + stainless faces; induction-ready, prémie |
Aplikácia: Lamp Reflectors and Lighting
Lighting is the second major market: the disc spins easily into a smooth reflector and accepts bright anodizing. Circles are spun into downlight housings, high-bay and street-light shades, floodlight bowls, spotlight cones and LED heatsink shells.
On a spinning lathe the disc flows over a mandrel into a seamless parabolic shell with a continuous optical surface; treated pure aluminum reflects roughly 85–90% of light and, being metallic, conducts heat away from the LED. Gauges are typically 0.4–1.2 mm. Larger or more rigid industrial shades may use anodized 1060 alebo 3003.
Spinning is preferred because the tooling is a single mandrel rather than a matched die set, so a factory can change shade shape at low cost and short lead time, and the process produces a seamless shell with no weld.
Deep bowls and deep-cone spotlights are almost always spun, while simple shallow housings may be stamped; the disc must be round, flat and gauge-consistent so the wall does not thin unevenly or split.
Reflectors are then chemically brightened or anodized, and the cleaner and purer the 1060 face, the higher the final reflectivity and the fewer defects show under a bright polish.
Aplikácia: Známky, Traffic Plates and Nameplates
1060 discs become circular traffic signs, regulatory and warning plates, road markers, elevator and equipment nameplates and plaques.
They are usually supplied in a half-hard or flat temper to keep a dent-free face, then screen-printed, eloxované, engraved or covered with reflective sheeting.
Pure aluminum weathers well and its anodic film holds color and print; plochosť, a clean surface and diameter tolerance are the priorities so the discs fit standard sign frames.
Circular signs are usually supplied in a flat, slightly firmer temper and in common frame diameters, with the edge left for the sign maker to roll or stiffen.
Reflectivity and weather resistance come from the applied sheeting and anodic film rather than the bare metal, so the priorities are a dent-free face, accurate diameter and a clean bonding surface; outdoor plates are commonly 1–2 mm thick to stay rigid in wind.
Aplikácia: Hardware, Electronics and Industrial Parts
1060 circles are also drawn, stamped or spun into a broad range of parts: cylindrical battery and capacitor shells for some cell formats (high-power cells often use 3003)
motor and instrument housings, filter and sieve discs, spun chemical-vessel heads, loudspeaker cones and dust caps, decorative spinnings, shims and heat-spreader discs.
Gauges can be as thin as 0.2–0.5 mm, with the emphasis on fine edges and a clean surface for subsequent plating, anodizing or bonding. Parts needing higher strength or pressure resistance should move to 3003 alebo 3004.
Many of these parts run at high volume with tight scrap allowances, so the same nesting, burr and flatness discipline used for cookware applies even though the discs are smaller, and an oil-free surface is essential when the part is later plated, anodized or bonded to seals.
A frequent mistake is stretching 1060 beyond its strength for a power-battery can or a pressurized housing; those jobs should use 3003 alebo 3004, confirmed from the part and its safety requirements rather than assumed.

Common Forming Defects and Troubleshooting
Most forming problems trace back to the blank’s gauge, miernosť, texture or surface.
| Defekt | Typical cause | Corrective action |
| Splitting at punch radius | blank too hard, draw ratio too high, tight radius, high holder force | use O temper, multi-draw, enlarge radius, tune holder, add lube |
| Flange / wall wrinkling | holder force too low, excessive clearance | increase holder force, correct clearance |
| Orange-peel surface | coarse grain from over-annealing | use fine-grain, correctly annealed coil |
| High earing / wavy rim | silná textúra, unsuitable rolling/anneal | use low-earing hot-rolled stock, increase trim allowance |
| Scoring / odieranie | rough die, poor lubrication, burr | polish die, improve lube, control edge |
| Spring-back / poor shape | blank too hard or wrong temper | use O or softer temper |
| Poťahovanie / anodizing defects | zvyškový olej, inklúzie, variable surface | specify oil-free clean surface, fine grain, fixed lot |
Kontrola kvality a normy
Quality control spans chemistry, mechanické správanie, forming performance and dimensions.
Spectrometers verify chemistry per heat; tensile tests confirm strength, yield and elongation; the Erichsen cupping test (good O stock often reaches 10–12 mm IE) measures stretch formability;
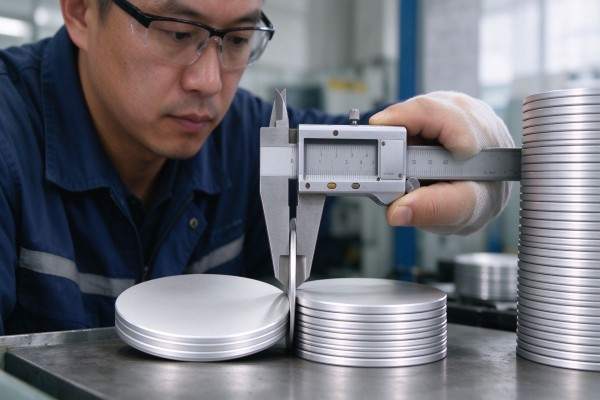
a drawn-cup test measures earing; and micrometers, calipers, straight-edges and surface inspection confirm gauge, priemer, plochosť, burr and the absence of roll marks, oil and pinholes.
Online thickness control, annealing furnace records and first-piece checks at blanking catch problems at the cheapest point.
Circles are supplied to GB/T 3880 (Čína), ASTM B209 (USA), IN 485/573 (Európe) or JIS (Japonsko), with a mill test certificate commonly to EN 10204 3.1.
Mills usually hold ISO 9001; food-contact parts are supported by FDA, Nariadenie EÚ 1935/2004 a 10/2011 a GB 4806, while lighting and electronics use RoHS/REACH declarations.
SGS or Bureau Veritas inspection can be arranged. Certificates should be issued for the specific lot.
| Štandardné / dokument | Účel |
| GB/T 3880 / ASTM B209 / IN 485 | zliatina, temper and dimensional compliance |
| MTC to EN 10204 3.1 | lot-specific chemistry and mechanical results |
| ISO 9001 | mill quality management system |
| FDA / EÚ 1935/2004 & 10/2011 / Gb 4806 | food-contact cookware compliance |
| RoHS / REACH | lighting and electronics compliance |
Incoming coil is checked against the heat and lot so any material with chemistry, gauge or surface deviation is segregated before it reaches the blanking press, and before packing sample discs are drawn into test cups to confirm earing and wall behavior.
This staged control stops a single out-of-spec coil being converted into thousands of defective parts. The MTC, the packing marks and the goods on the pallet should all carry the same lot reference so a problem can be traced back to the exact coil.
Custom Production, Packaging and Logistics
Suppliers customize diameter, hrúbka, miernosť, casting route and surface (mill, leštený, kefovaný, anodized or pre-coated), edge condition and packing, including private labels.
A new diameter needs a blanking die, so first orders involve tooling and a production-gauge sample that the customer draws and coats; the signed sample becomes the receiving standard for repeat lots.
Circles are interleaved or filmed, palletized and moisture-proof wrapped for sea freight, with FOB/CFR/CIF terms and 30% T/T deposit plus balance against the bill of lading (L/C at sight for large orders).
The document set includes the bill of lading, invoice, baliaci zoznam, MTC and certificate of origin, with food-contact or RoHS declarations as needed.
Aluminum is also fully recyclable: the nesting skeleton and production scrap are re-melted without losing properties, and recycled aluminum needs only a small fraction of the energy used for primary metal.
A line that recovers its offcuts therefore lowers both waste and embodied metal, which matters for cookware and lighting brands that report recycled content; a traceable mill can supply scrap-recovery and lot records on request.
Pricing and Cost Drivers
Circles are priced as the aluminum ingot price plus a processing fee, per ton or per piece. The metal base follows the daily LME and the Chinese Shanghai futures and spot quotations, so fixed online prices are only indicative and a valid quote is re-validated against the day’s ingot price and confirmed specification.
| Cost factor | Effect on price |
| Ingot price | metal base, varies daily with LME / Shfe |
| Nesting yield | higher utilization (70s–mid 80%) lowers per-piece cost |
| Rozmer / priemer | very thin or very thick gauges and unusual diameters add cost |
| Temper / casting route | annealed O and hot-rolled low-earing stock cost more |
| Povrch / tolerancie | leštenie, anodizing and tight tolerances add cost |
| Množstvo / doručenie | container volumes spread tooling; packaging and freight add cost |
Buyers lower cost by standardizing common diameters, ordering full containers, taking mill finish where the part will be coated, and sourcing from a mill that blanks its own coil at high yield. Quotations far below market usually reflect the wrong temper, a poor casting route or loose gauge rather than a genuine saving.
Export quotes are usually FOB, CFR or CIF: FOB covers the goods to the named Chinese port, CFR adds ocean freight, and CIF adds insurance as well, so compare on the same basis.
Because the metal base moves daily, every quote carries a validity window of a few days and the price is re-confirmed on the day the deposit is paid.
A credible supplier shows the ingot basis and processing fee separately and provides a pro-forma invoice listing specification, tolerancie, povrch, packing and gross/net weight, removing ambiguity before production.
Choosing a Manufacturer and How to Order
The key distinction is a rolling-and-blanking mill versus a trader: the mill controls the coil, annealing and blanking and can guarantee chemistry, miernosť, earing and traceability, while a trader is convenient for small mixed orders but cannot control the upstream process. China’s circle industry is concentrated in Henan (Gongyi/Zhengzhou) and Shandong (Pingyin/Liaocheng), close to the cookware clusters in Zhejiang and Guangdong. Verify in-house capability, the casting route and temper, lot-specific certificates and a production-gauge sample drawn on your own line, then sign a sample standard.
- Inquiry and specification: send the alloy, miernosť, hrúbka, priemer, množstvo, povrch, štandardné, destination and a drawing or sample disc.
- Citácia: the supplier confirms the blank diameter, casting route, meradlo, price basis and validity.
- Tooling and samples: a new diameter is tooled and production-gauge samples are blanked for draw and coating trials.
- Sample approval: you form the samples and sign a pre-production standard.
- Deposit and scheduling: a 30% deposit is paid and the lot is scheduled for rolling, annealing and blanking.
- Production and inspection: the lot is produced, tested and documented; third-party inspection can be arranged.
- Packing and loading: discs are interleaved, paletizované, wrapped and loaded for export.
- Balance and shipment: the balance is paid against the bill of lading and the documents are released.
Repeat orders are much faster because the tooling, signed sample and approved specification already exist, so the mill only slots the run into its plan. Complete information and prompt sample approval are what most shorten a first order.
Lead time depends on tooling, gauge and quantity; trial lots and forming samples are available. To start, request a quote with the drawing, priemer, hrúbka, temper and quantity for a factory-direct quotation and samples.
O ekologickom kameni
Eco Alum is an aluminum product supplier established in March 2025, organized around a rich supply chain within China’s aluminum rolling industry.
Instead of acting as a simple trader, we coordinate with qualified rolling and blanking mills to deliver specification-accurate material at factory-direct pricing and manage the technical, quality and export documentation.
Our main products are aluminum plates, cievky, fólie, strips and discs (kruhy), covering the 1xxx series—1050, 1060, 1070, 1100, 1235 and 1350—along with alloys such as 3003.
Pre 1060 circles we supply custom gauges, diameters, tempers and surfaces for cookware, osvetlenie, sign and hardware converters, with hot-rolled low-earing stock on request, mill test certificates, sample approval, moisture-proof export packing and complete shipping documents.
We help you choose between 1060, 1050 a 3003 for the specific part rather than selling one alloy for every application. Reach us at [email protected] or +86 19924932491.
We support buyers with drawings and blank-size guidance, production-gauge forming samples before a first order, lot-specific mill certificates and compliance documents, and moisture-proof export packing with complete customs paperwork.
For cookware converters we also advise on hot-rolled versus cast-rolled stock, the correct O temper for the draw depth and the surface finish that matches your coating line. Send your drawing or sample disc to [email protected] for a prompt, specification-based quotation.
Často kladené otázky
Q: What are 1060 aluminum circles used for?
A: Mostly deep-drawn and spun cookware (non-stick pans, pressure cookers, hrnce, kettles), plus lamp reflectors, znaky, menové štítky, battery/capacitor cans and stamped hardware.
Q: What sizes can be supplied?
A: About 0.2–6 mm thick and 80–1200 mm in diameter, cut to tooling; cookware discs are usually 0.5–4 mm and 100–400 mm.
Q: Which temper is best for deep drawing?
A: The soft O temper gives the highest draw ratio and is the cookware standard; H12/H14/H22/H24 suit shallow forms and stiffer spinnings.
Q: 1060 alebo 3003 for cookware?
A: 1060 is the economical, easy-to-coat body for most pans; 3003 is ~15–20% stronger for pressure cookers and clad/induction parts.
Q: Hot-rolled or cast-rolled stock?
A: Valcované za tepla (DC) has lower earing and better deep drawing for tall cookware; twin-roll cast stock is more economical for shallow and medium parts.
Q: How is price calculated?
A: Ingot price plus a processing fee, driven by nesting yield, meradlo, miernosť, surface and quantity, following the daily LME/Shanghai spot and re-validated at order time.
Q: Je 1060 magnetic and induction-ready?
A: No—1060 is non-magnetic. Induction cookware uses a clad disc with a magnetic stainless steel base bonded to the aluminum, or a separate induction plate on the bottom.
Q: What is the MOQ and can I get samples?
A: Trial lots and production-gauge forming samples are available. A new diameter needs a blanking die, and full containers are the most economical for repeat production.
Záver
1060 aluminum circles are the press-ready backbone of the cookware and spun-lighting industries and a versatile blank for signs, hardware and cans.
The application sets the specification: soft O and hot-rolled low-earing stock for deep cookware, bright discs for reflectors, a flat half-hard blank for signs, a 3003/3004 where strength or pressure is involved.
Sourcing from an in-house rolling-and-blanking mill, verifying certificates and earing, and approving production-gauge samples delivers the best yield and forming consistency at the lowest landed cost.
Skrátka, the specification follows the application rather than the alloy name: mäkký, low-earing, clean-surface blank for deep cookware and reflectors, a flat firmer blank for signs, and a manganese alloy for pressure or strength.
Once the blank is fixed, tooling is opened and a sample signed, supply becomes repeatable and the remaining variables—ingot price and freight—can be managed transparently. Eco Alum is set up to make that first specification correct and to keep repeat lots consistent.


